 Posted by
Introduction: The Supply Puzzle Behind a Simple Wardrobe
Define the core idea first: a wardrobe only looks simple once it is on the retail floor. In reality, wardrobes supply must balance design fidelity, stable lead times, and low damage rates across many partners. Picture a store manager entering peak season with a forecast spike and a narrow receiving window—then ask, how do they stay in stock without paying for excess storage or rush freight? Recent trade data shows average lead times still hover near 10–14 weeks for cross-border shipments, while return rates rise when kits are mispacked or hardware assortments drift by even 1%. If a fast-selling SKU misses its slot, switching costs surge and customers drop off (the aisle does not wait). So, is the real bottleneck production capacity, packaging precision, or the way teams define the bill of materials and handoffs?
We’ll map the question to real choices, side-by-side, and build toward an evidence-based answer.
Wardrobe Wholesale: Where the Hidden Friction Actually Lives
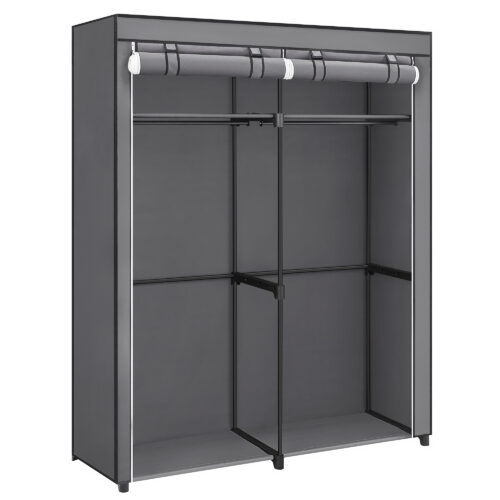
wardrobe wholesale at scale promises simple savings, yet the pressure points are not where most buyers look. The top risk is not unit price—it’s variance. A kit can meet price targets and still fail on fit if the edge banding is thin, the cam locks mismatch, or the carton crush rating is off by a notch. That is how damage rates creep past 3% and wipe out margins. BOM drift also sneaks in when alternate hinges look “equivalent” but alter door alignment under load. Add container mix rules, and packing density drops. Look, it’s simpler than you think: standardize what matters, then test to failure before you buy big. Terms to watch: SKU rationalization, CNC routing tolerances, melamine-faced chipboard (MFC) moisture class, and flat-pack logistics. A small miss in any one will echo through receiving, assembly time, and returns—funny how that works, right?
Where do costs really hide?
They hide in rework minutes, not spreadsheets. A kit that assembles five minutes faster scales to hours saved per pallet across stores. They hide in carton design when corner crush protection is 5% under spec and leads to invisible edge cracks. They hide in forecasting when minimum order quantities force overbuy, then push markdowns. Traditional fixes—bigger safety stock, broader assortments—stretch cash and add noise. Better fixes align process: run pilot builds; instrument damage at the part level; track OTIF; and verify that the hardware pack is version-locked to the CAD. Bring in JIT buffers only after you stabilize the upstream laminate press and drilling cell. Keep a tight BOM and spec sign-off, and enforce it with first-article inspection and ERP change control. Short story: control variance first, price second—and your wholesale deal starts to feel like a strategy, not a gamble.
From Bulk Buys to Smart Flow: What Changes Next
What’s Next
The next wave is technical, and it compares old levers to new ones. Yesterday, buyers traded MOQs against unit cost. Tomorrow, demand sensing links store-level signals to factory slots, so forecasts update weekly and cut dead stock. Digital twins of key SKUs let teams simulate hardware swaps and carton stacking before a single board is cut—so design-to-assembly friction drops. CAD-to-CAM pipelines push final specs to CNC routing with fewer operator touches, while edge quality is validated with inline vision checks. Leading bedroom wardrobe manufacturers now tag pallets with RFID and stream receiving data into ERP for real-time OTIF and damage-per-1,000 metrics. Even simple sensors at edge nodes in the warehouse track humidity, which helps keep MFC panels within tolerance. The result is not magic; it is fewer surprises. Fewer surprises mean steadier cash flow—and yes, that matters.
Compare outcomes head-to-head. Old model: negotiate hard, stock deep, and accept 2–4% damage as a cost of doing business. New model: design for assembly, validate packaging with ISTA protocols, and buy flexible capacity with tiered lead times. Old model: monthly reviews on a broad assortment. New model: SKU rationalization guided by return analytics and assembly time studies. This is how teams shift from firefighting to control. It also reframes supplier conversations: talk in measurable targets (assembly minutes per unit, carton failure rates, spec compliance), not only in dollars per piece. Summarizing the thread so far, price gaps matter, but variance kills throughput. Processes that lock the BOM, monitor pack integrity, and sync schedules reduce total landed cost more than a simple discount ever will.
Before you commit, weigh solutions with three clear metrics. 1) Spec adherence rate: percent of lots passing first-article inspection with zero deviations in hardware kits and finishes. 2) Damage and rework index: verified defects per 1,000 units from receiving to customer assembly, including time-to-fix minutes. 3) Flow reliability: OTIF by lane, plus lead-time delta versus forecast under stress events. Track these for two cycles, and the right supplier path will surface. That is the practical edge in a market that looks crowded but rewards discipline. And when you need a reference point for consistent practice and catalog depth, see SONGMICS HOME B2B.